 Australia
 Canada
 Cayman Islands
 Dominican Republic
 Hong Kong
 India
 Indonesia
 Ireland
 Jamaica
 New Zealand
 Singapore
 United Kingdom
 United States
 Vietnam
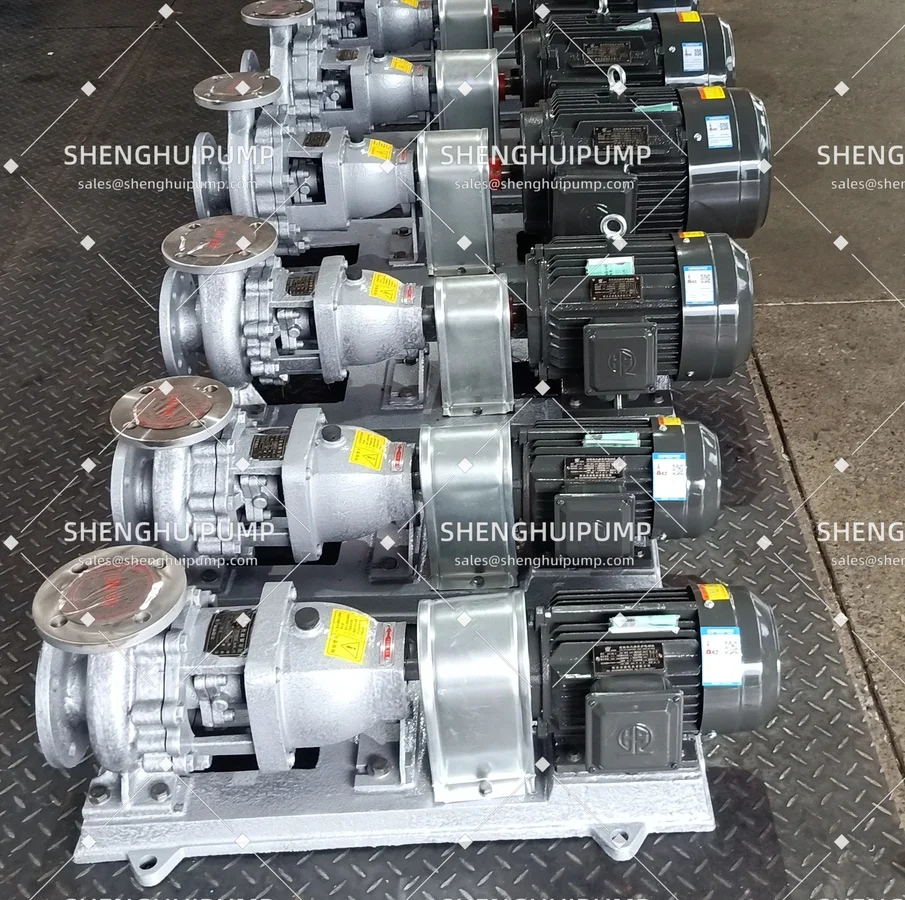
In chemical manufacturing, the performance of fluid transfer equipment can directly affect production continuity, operating costs, and workplace safety. Moving corrosive liquids between storage tanks, processing equipment, and production lines requires more than sufficient pumping capacity. The equipment must also withstand demanding operating conditions while maintaining stable flow and minimizing maintenance interruptions. This is where the IH Series Chemical Centrifugal Pump offers practical advantages for industrial applications.
Designed for the transportation of chemical liquids, the IH series combines corrosion-resistant construction with a straightforward mechanical structure. Its horizontal, single-stage, single-suction configuration makes it suitable for a wide range of industrial fluid transfer operations. For chemical plants seeking dependable pumping equipment without unnecessary mechanical complexity, the IH series provides an effective balance between performance, durability, and maintenance accessibility.
Corrosion-Resistant Construction for Demanding Chemical EnvironmentsOne of the biggest challenges in chemical processing is the deterioration of equipment caused by prolonged exposure to aggressive liquids. Acids, alkaline solutions, and other chemical compounds can gradually damage unsuitable pump components, leading to leakage, reduced performance, and unexpected shutdowns.
IH stainless steel chemical centrifugal pump is designed to address these challenges through its corrosion-resistant wetted components. Depending on the stainless steel grade and the chemical properties of the liquid, the pump can be used for transferring a variety of corrosive and non-corrosive media.
This material construction is particularly valuable in chemical production facilities where pumps operate frequently and come into contact with process liquids over extended periods. Suitable material compatibility helps reduce corrosion-related deterioration and supports longer equipment service life.
Stable Liquid Transfer Supports Continuous ProductionChemical production often involves multiple interconnected processes, including raw material preparation, chemical reactions, filtration, and liquid storage. An interruption in one pumping stage can affect the operation of an entire production line.
IH centrifugal pump uses a single-stage impeller to transfer mechanical energy from the motor to the liquid. As the impeller rotates, liquid enters through the axial suction inlet and is accelerated outward before leaving through the radial discharge outlet.
This operating principle allows the pump to deliver continuous fluid movement under appropriate operating conditions. Its hydraulic configuration is well suited to industrial processes that require consistent liquid circulation and transfer.
In chemical plants, stable pumping performance can help maintain process flow, support reliable liquid delivery between equipment, and reduce disruptions caused by irregular fluid transportation.
Supporting Efficient Operation and Lower Operating CostsEnergy consumption is an important consideration for chemical manufacturers, particularly in facilities where pumps operate for long periods each day.
IH horizontal centrifugal pump is designed to provide efficient hydraulic performance through its centrifugal pumping mechanism and coordinated impeller and casing structure. When operated near its intended duty point, the pump can transfer liquids effectively while limiting unnecessary energy losses.
Its corrosion-resistant construction and serviceable mechanical arrangement also contribute to overall operating economy. Reduced corrosion-related damage, manageable maintenance requirements, and reliable liquid transportation can help lower the total cost of pump ownership.
Versatile Applications Across Industrial ProcessingAlthough the IH series is primarily associated with chemical manufacturing, its applications extend to several other industrial sectors.
In chemical plants, the pump can be used for transferring compatible acids, alkaline solutions, chemical intermediates, and process liquids between storage tanks and production equipment. It can also support liquid circulation in selected chemical processing systems.
In petroleum and petrochemical facilities, the IH series can handle compatible liquid chemical additives and process fluids where its material construction, sealing arrangement, and operating specifications meet application requirements.
Metallurgical and industrial processing facilities may use these pumps for transferring compatible cooling liquids, treatment solutions, and other process media. The pump can also serve selected water treatment and industrial wastewater applications involving liquids within its hydraulic and material limitations.
A Dependable Pumping Solution for Chemical ProcessingAs chemical manufacturing becomes increasingly focused on operational efficiency and equipment reliability, the importance of dependable fluid transfer systems continues to grow.
IH series chemical transfer pump offers a practical combination of corrosion resistance, stable hydraulic performance, structural simplicity, and industrial versatility. By supporting continuous liquid transfer and manageable maintenance, it can help chemical plants improve operational reliability and control long-term equipment expenses.
For chemical manufacturers, engineering contractors, and industrial equipment distributors looking for reliable chemical pumping solutions, the IH series remains a valuable option for a wide range of compatible fluid transfer applications.
Looking for a reliable chemical centrifugal pump manufacturer?
Shenghui Pump provides industrial pumping solutions for chemical processing and other demanding applications. Explore our IH Series Chemical Centrifugal Pumps and contact us for product information, technical specifications, and quotations.
Website: www.shenghuipump.com